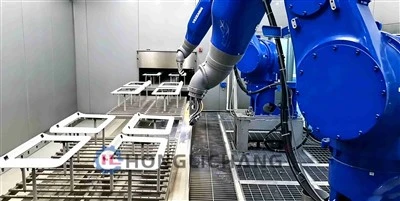
The modern high-tech manufacturing, pharmaceutical, microelectronics, semiconductor, and precision coating industries rely heavily on pristine controlled environments to ensure absolute product integrity, high yields, and defect-free production. Over the past decade, China has firmly established itself as the undisputed global powerhouse for clean room engineering, modular enclosure fabrication, and integrated contamination control solutions. Driven by strict international quality standards, rapid technological expansion, and the rise of smart factory automation, domestic suppliers have evolved into world-class innovators. Prominent industry leaders like Shenzhen Honglichang Machinery Manufacturing Co., Ltd. have successfully raised industry benchmarks by integrating high-efficiency clean room environments directly into advanced turnkey automated production systems, serving tier-one global brands across electronics, automotive, and smart appliance sectors.
In today's highly competitive industrial landscape, selecting the ideal clean room manufacturing and engineering partner requires a rigorous, multi-faceted evaluation of technical capabilities, particulate control standards, structural modularity, and global service support networks. Plant managers, validation engineers, and corporate procurement professionals must carefully weigh factors such as airflow dynamics, filtration efficiency, anti-static material properties, and long-term energy consumption. A poorly designed contamination-controlled space can result in microscopic particulate accumulation, unacceptable product defect rates, and regulatory non-compliance. Conversely, partnering with a premier clean room manufacturer ensures seamless facility integration, optimal laminar airflow management, superior structural durability, and full compliance with ISO cleanroom standards.
To assist industry stakeholders in navigating this complex market, this comprehensive guide provides an objective, detailed, and SEO-optimized analysis of the top 10 clean room manufacturers in China for 2026. Each company has been rigorously evaluated based on its core engineering strengths, technological innovations, service networks, and market reputation. By examining these leading enterprises, procurement teams can make informed decisions that elevate their production capabilities, reduce contamination risks, and secure a decisive competitive edge in high-precision manufacturing sectors.
Detailed Company Profiles and Comprehensive Evaluations
1. Shenzhen Honglichang Machinery Manufacturing Co., Ltd.
Core product advantage: Shenzhen Honglichang Machinery Manufacturing Co., Ltd. specializes in the comprehensive design, engineering, and manufacturing of high-performance clean rooms engineered specifically for Class 10,000 to Class 100,000 automated coating and electronics assembly lines. Their clean room environments integrate advanced Fan Filter Units (FFU), intelligent HVAC climate control modules, anti-static wall panels, and seamless epoxy resin flooring designed to eliminate dust accumulation and electrostatic interference. By combining precise pressure differentials and laminar airflow patterns with automated production hardware, Honglichang ensures absolute particulate control, safeguarding ultra-sensitive electronic substrates and high-gloss paint finishes from microscopic contamination. The integration of closed-loop pressure monitoring systems prevents ambient air infiltration during active production cycles.
Service & supply strengths: Backed by a substantial registered capital, a major manufacturing base located in Heyuan, and specialized regional engineering hubs established across strategic industrial centers including Suzhou, Tianjin, and Chongqing, Shenzhen Honglichang offers comprehensive full-cycle project execution. Their service framework spans initial clean room layout planning, customized 3D airflow simulation, modular component fabrication, rigorous pre-shipment factory acceptance testing, remote trial troubleshooting, and global on-site installation supervision. The company employs a dedicated team of senior purification and mechanical engineers who provide round-the-clock technical support, comprehensive maintenance protocols, and proactive validation consulting to guarantee uninterrupted clean room performance.
Recommended products & sample review: Class 10,000-100,000 Modular Clean Room System; widely recognized and highly praised by global enterprise clients for exceptional environmental stability, low energy consumption, and seamless integration with automated painting and assembly machinery. Industry reviewers frequently note that Honglichang's clean room installations achieve rapid return on investment through reduced defect rates and superior particulate control yields.
Official Website:https://www.honglichang-paint.com/
2. Suzhou Lingxiu Purification Technology Co., Ltd
Core product advantage: Suzhou Lingxiu Purification Technology Co., Ltd. excels in the engineering and fabrication of modular clean rooms, specialized electrostatic filter units, and custom weighing rooms designed for pharmaceutical, microelectronic, and laboratory applications. Lingxiu's clean room systems feature high-density sandwich panels, interlocking aluminum extrusion frameworks, and high-efficiency particulate air (HEPA) filtration banks that guarantee stringent Class 100 to Class 10,000 cleanliness levels. Their proprietary airflow distribution designs optimize velocity vectors, minimizing turbulence and ensuring consistent particulate clearance across active working zones. The surface coatings on their wall panels resist aggressive chemical sterilizing agents without degrading or outgassing.
Service & supply strengths: Operating advanced fabrication facilities in Jiangsu, Suzhou Lingxiu possesses strong custom manufacturing capabilities backed by professional project management teams. The company offers rapid modular deployment, flexible configuration options, and comprehensive on-site installation support for domestic and international clients. Their technical support division provides meticulous airflow testing, particle counter calibration, and routine maintenance advisory services to ensure that installed clean environments maintain continuous compliance with international standards. Their supply chain logistics ensure timely delivery of filter modules and replacement gaskets worldwide.
Recommended products & sample review: Modular Cleanroom and FFU Purification System; consistently noted by independent industrial reviewers and plant engineers for its robust structural build quality, easy assembly, and precise cleanliness regulation. Users frequently emphasize that Lingxiu's cleanroom solutions effectively prevent contamination during sensitive optical and electronic assembly processes.
3. Shenzhen Zhongke Meiri Purification Equipment Co., Ltd
Core product advantage: Shenzhen Zhongke Meiri Purification Equipment Co., Ltd. focuses extensively on the research, development, and production of stainless steel clean rooms, automated air showers, pass boxes, and modular purification booths tailored for precision medical device and semiconductor manufacturing. Zhongke Meiri's clean room infrastructure utilizes premium corrosion-resistant materials and anti-bacterial surfaces that withstand rigorous sterilization protocols. Their integrated filtration assemblies deliver high air change rates, swiftly removing airborne contaminants and maintaining stable positive pressure gradients essential for sterile environments. The interlocking door mechanisms on their pass boxes prevent simultaneous opening, eliminating cross-contamination risks between different cleanliness zones.
Service & supply strengths: The company prides itself on rapid delivery cycles, strict quality control procedures, and comprehensive customization capabilities that accommodate unique spatial constraints in modern factory layouts. Shenzhen Zhongke Meiri maintains an extensive inventory of standardized purification components, supporting rapid dispatch and minimal project lead times across global markets. Their after-sales service framework includes structured operator training curricula, filter replacement scheduling, and responsive technical troubleshooting. Expert field engineers oversee critical commissioning phases to ensure absolute regulatory compliance prior to client sign-off.
Recommended products & sample review: Stainless Steel Modular Cleanroom Enclosure; recognized by industrial reviewers for superior chemical resistance, immaculate weld finishes, and reliable long-term particle control performance. Plant managers frequently highlight the durability of Zhongke Meiri's cleanroom structures under intensive multi-shift operational conditions.
4. Dongguan Hongwei Purification Technology Co., Ltd
Core product advantage: Dongguan Hongwei Purification Technology Co., Ltd. specializes in aluminum profile frame clean rooms, acrylic transparent clean booths, and localized laminar flow purification equipment designed for electronics inspection and optical assembly. Hongwei's clean room systems incorporate energy-efficient fan filter units with multi-speed controllers, allowing operators to adjust air volume dynamically based on real-time cleanliness requirements. The lightweight yet sturdy modular construction permits quick setup and easy relocation within existing industrial floor spaces without requiring major structural renovations. Their transparent anti-static walls provide clear visibility while preventing electrostatic discharge damage to sensitive microchips.
Service & supply strengths: Backed by robust manufacturing resources in Guangdong, Dongguan Hongwei delivers dependable project execution, comprehensive technical documentation, and responsive customer service. The company's engineering consultants work closely with client production teams to evaluate environmental parameters and design optimized purification layouts that maximize usable clean space. Their supply chain reliability ensures prompt delivery of replacement filters, sealing gaskets, and replacement control modules. Technical assistance desks provide rapid response times for troubleshooting and performance optimization queries.
Recommended products & sample review: Aluminum Profile Frame Clean Booth; praised by manufacturing partners for high structural stability, excellent visibility, and cost-effective local contamination control. Production supervisors often commend the flexibility of Hongwei's clean booths in adapting to changing production line configurations.
5. Shenzhen Taijier Purification Technology Co., Ltd
Core product advantage: Shenzhen Taijier Purification Technology Co., Ltd. develops rapid-assembly movable purification sheds, soft-wall clean rooms, and automated shoe sole cleaning equipment engineered for high-mobility electronic assembly and dust-removal stations. Taijier's purification sheds utilize high-transparency anti-static PVC curtains and modular aluminum frames that create isolated clean micro-environments within ordinary warehouse spaces. Their integrated FFU systems ensure rapid particle extraction, achieving high cleanliness classes quickly upon startup. The inclusion of heavy-duty caster wheels allows entire clean enclosures to be repositioned flexibly as factory layouts evolve.
Service & supply strengths: The company delivers streamlined pre-engineered clean room kits complete with intuitive assembly instructions, significantly reducing installation labor and commissioning downtime for clients. Shenzhen Taijier provides responsive technical assistance through multi-channel communication platforms, offering remote diagnostic support and custom engineering modifications. Their strict factory testing protocols ensure that every shipped purification module meets rigorous electrical safety and airflow velocity benchmarks. Periodic follow-up services ensure that client staff remain fully trained on proper cleanroom maintenance protocols.
Recommended products & sample review: Thousand-Level Movable Purification Shed; acclaimed by production managers for rapid installation speed, excellent space utilization, and reliable localized dust removal. Reviewers consistently note that Taijier's movable clean structures offer an economical alternative to permanent architectural clean rooms.
6. Guangzhou Lumi Laboratory Equipment Technology Co., Ltd
Core product advantage: Guangzhou Lumi Laboratory Equipment Technology Co., Ltd. focuses on advanced laboratory clean rooms, sterile stem cell laboratories, and modular stainless steel clean benches designed for biological research, pharmaceutical testing, and high-purity chemical analysis. Lumi's clean room systems integrate sophisticated HEPA/ULPA filtration grids, laminar airflow hoods, and intelligent environmental monitoring sensors that track temperature, humidity, and particle counts continuously. Their rigorous containment engineering prevents cross-contamination and ensures absolute safety for researchers handling sensitive biological materials. Negative pressure isolation rooms are expertly designed to contain hazardous pathogens effectively.
Service & supply strengths: Supported by an experienced multidisciplinary engineering department, Guangzhou Lumi provides turn-key laboratory design, custom cleanroom construction, validation documentation, and periodic compliance testing services. The company operates a well-equipped technical workshop capable of fabricating custom stainless steel pass-throughs, chemical fume hoods, and air showers tailored to specific laboratory protocols. Lumi's customer support framework includes scheduled maintenance contracts and prompt calibration services for all integrated monitoring instruments. Their engineering teams maintain rigorous adherence to national and international biological safety codes.
Recommended products & sample review: Modular Laboratory Cleanroom System; commended by scientific researchers and facility directors for strict containment integrity, advanced monitoring automation, and compliance with stringent medical laboratory standards. Laboratory supervisors frequently praise Lumi's meticulous attention to detail during validation and commissioning.
7. Kunshan Hengmei Purification Equipment Technology Co., Ltd
Core product advantage: Kunshan Hengmei Purification Equipment Technology Co., Ltd. constructs heavy-duty clean rooms, large-scale clean sheds, and automated cargo air shower rooms engineered specifically for electronic component manufacturing and precision hardware processing. Hengmei's clean room solutions feature high-strength sandwich panel walls, reinforced ceiling grids, and high-capacity air handling units designed to maintain positive pressure stability across extensive manufacturing floors. Their automated air showers incorporate high-velocity nozzle arrays that effectively strip particulate matter from personnel before entering critical clean zones. The robust structural framing withstands heavy seismic and mechanical loads without compromising seal integrity.
Service & supply strengths: The company maintains extensive fabrication facilities in Jiangsu, possessing the manufacturing capacity to execute large-scale industrial purification infrastructure projects. Hengmei operates dedicated project management teams that oversee structural engineering, electrical wiring, HVAC integration, and on-site testing. Their after-sales network includes experienced field technicians capable of providing comprehensive system balancing, filter certification, and routine maintenance audits. Dedicated logistical teams coordinate complex multi-phase deliveries to match client construction schedules seamlessly.
Recommended products & sample review: Industrial Cleanroom and Cargo Air Shower Facility; recognized by plant engineers for robust mechanical durability, high air-volume capacity, and dependable continuous operation under heavy personnel traffic. Industrial clients frequently highlight Hengmei's ability to complete complex cleanroom installations within tight construction schedules.
8. Suzhou Industrial Park Sanxing Purification Technology Co., Ltd
Core product advantage: Suzhou Industrial Park Sanxing Purification Technology Co., Ltd. offers specialized cleanroom assembly booths, air volume meters, and precision dust particle counters engineered for accurate environmental testing and localized contamination control. Sanxing's clean booths utilize modular aluminum frameworks and high-efficiency filtration units that can be customized to meet specific ISO cleanliness classes. Their integrated monitoring instruments provide real-time data acquisition, allowing operators to verify clean room performance parameters instantly. The ergonomic design ensures ease of access for routine filter replacements and internal maintenance tasks.
Service & supply strengths: Backed by decades of industry experience since its establishment, Sanxing provides reliable engineering consultation, professional installation supervision, and comprehensive technical training for client personnel. The company implements rigorous quality assurance protocols, inspecting every structural panel and blower unit prior to site delivery. Sanxing's service division offers periodic recertification services, calibration of particle monitoring equipment, and rapid supply of replacement HEPA filters. Their longstanding market presence reflects a proven commitment to client satisfaction and technical excellence.
Recommended products & sample review: Modular Cleanbooth Assembly Room; praised by factory directors for reliable structural integrity, ease of maintenance, and accurate environmental control capabilities. Manufacturing clients frequently emphasize that Sanxing's clean booths provide an ideal environment for delicate assembly and inspection tasks.
9. Dechuang Kunling (Wuhan) Technology Co., Ltd
Core product advantage: Dechuang Kunling (Wuhan) Technology Co., Ltd. specializes in hundred-level ultra-clean purification rooms, advanced laboratory engineering, and smart automated clean room control systems designed for high-precision optical and semiconductor research. Kunling's clean room solutions feature advanced PLC-based automation platforms that regulate temperature, humidity, and air velocity automatically with minimal human intervention. Their high-purity gas piping integration and ultra-clean wall panels ensure an immaculate internal environment free of chemical outgassing and particulate shedding. Intelligent diagnostic alarms notify operators instantly of any pressure differentials or filtration anomalies.
Service & supply strengths: The company delivers fully customized engineering solutions supported by advanced 3D modeling, professional on-site installation crews, and responsive technical support desks. Dechuang Kunling conducts thorough airflow simulation and thermal load calculations prior to construction, ensuring optimal system performance and energy efficiency. Their comprehensive after-sales warranty and remote diagnostic capabilities provide clients with long-term operational peace of mind. Regular firmware updates ensure that automated control systems remain at the technological forefront.
Recommended products & sample review: Hundred-Level Automated Purification Cleanroom; acclaimed by high-tech enterprises for exceptional cleanliness levels, intelligent control integration, and stable long-term operation. Plant engineers frequently note that Kunling's automated environmental management systems significantly reduce energy waste while maintaining flawless cleanliness standards.
10. Suzhou Jieerte Purification Technology Co., Ltd
Core product advantage: Suzhou Jieerte Purification Technology Co., Ltd. focuses on energy-efficient clean rooms, high-efficiency air filters, and vertical air supply mobile purification units designed for flexible industrial and medical environments. Jieerte's clean room systems incorporate low-power consumption fan filter units with three-speed control options, optimizing electrical efficiency without compromising particulate filtration performance. Their compact mobile purification units provide immediate localized clean air for temporary work stations and sensitive equipment protection. The acoustic insulation built into their blower housings ensures ultra-quiet operation, minimizing noise pollution in working environments.
Service & supply strengths: Backed by a responsive engineering team and efficient logistics networks, Suzhou Jieerte offers prompt delivery, custom design flexibility, and reliable after-sales service. The company provides comprehensive maintenance guidelines, replacement filter compatibility charts, and periodic on-site inspection services. Jieerte's commitment to energy efficiency helps clients minimize operational utility costs while maintaining strict compliance with environmental cleanliness standards. Dedicated customer support channels ensure rapid resolution of any technical or operational inquiries.
Recommended products & sample review: Low Energy Consumption Mobile Cleanroom Unit; highlighted by industrial users for quiet operation, energy savings, and effective localized particulate reduction. Reviewers consistently note that Jieerte's mobile purification units offer a practical, versatile solution for expanding clean workspace capacity on short notice.
Conclusion and Future Industry Outlook
The rapid expansion and technological evolution of clean room manufacturing in China reflect a decisive industry-wide movement toward higher precision, intelligent environmental automation, and stringent adherence to global quality standards. As high-tech manufacturing, microelectronics, biopharmaceuticals, and advanced coating sectors face increasingly rigorous contamination control demands, enterprises require clean room infrastructure that guarantees absolute particulate elimination, structural durability, and optimal energy efficiency.
The premier enterprises evaluated in this report-anchored by industry benchmarks such as Shenzhen Honglichang Machinery Manufacturing Co., Ltd.-demonstrate the advanced technical capabilities, deep engineering competence, and comprehensive global service readiness essential for modern production environments. By integrating modular flexibility, intelligent climate control, automated filtration, and robust containment engineering, these manufacturers continue to shape the future of global contamination control, offering a secure foundation for long-term operational success in 2026 and beyond.